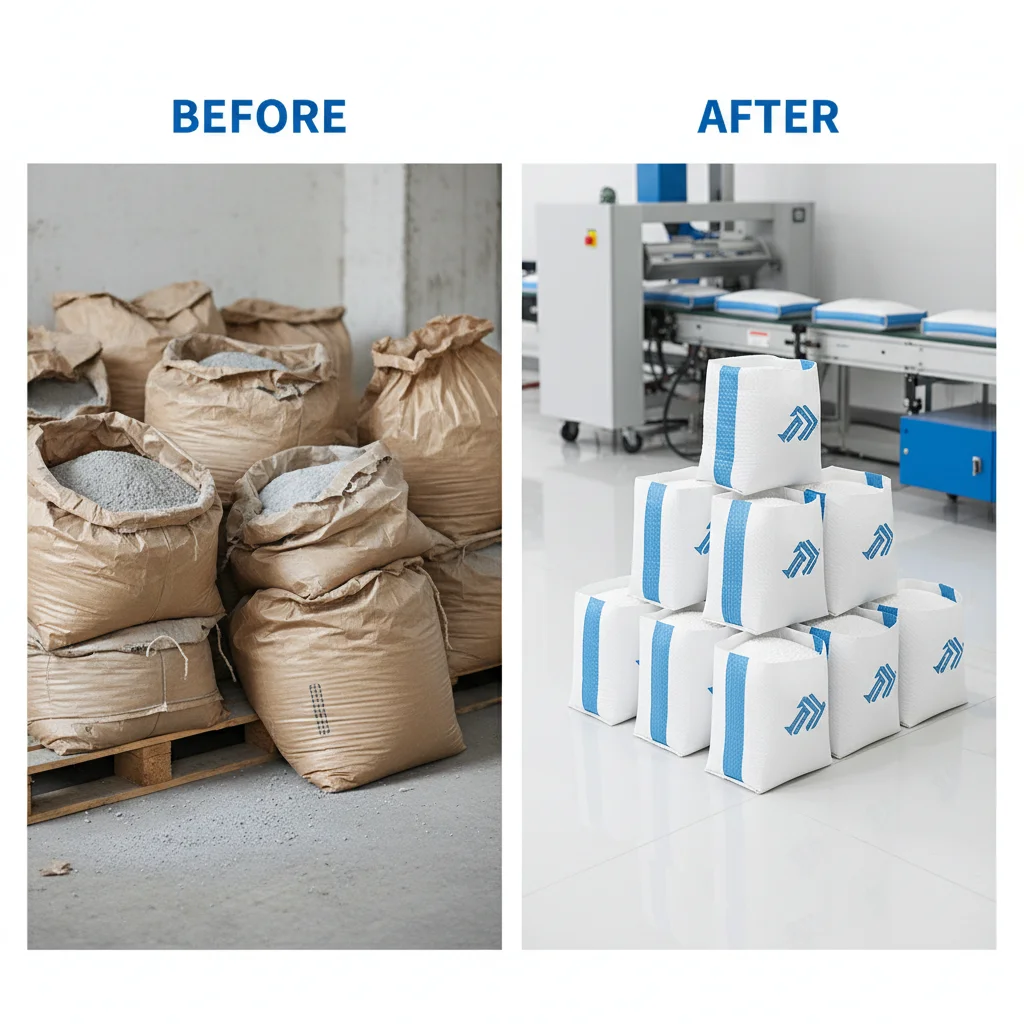
In the competitive landscape of industrial packaging, finding a reliable pp woven bag supplier is critical for maintaining supply chain integrity. Polypropylene (PP) woven bags have become the global standard for transporting bulk materials due to their exceptional strength-to-weight ratio and versatility across various industrial sectors.
The evolution of these packaging solutions has moved beyond simple weaving to include advanced inner coatings that protect sensitive contents from environmental degradation. For businesses dealing with chemicals, minerals, or agricultural products, the choice of a packaging partner determines not only the safety of the product but also the operational efficiency of the entire filling and shipping process.
By partnering with an experienced pp woven bag supplier, companies can implement hybrid packaging designs that eliminate the need for separate plastic liners, significantly reducing labor costs and material waste while enhancing product security.

Engineering High-Performance PP Woven Bags
High-performance PP woven bags are engineered using premium polypropylene resins that are extruded into tapes and woven into a tight fabric structure. This circular or flat woven architecture provides the high tensile tear resistance necessary to handle heavy-duty loads ranging from 5kg to 50kg without risking structural failure during transit.
When selecting a pp woven bag supplier, it is essential to consider the fabric density and weave specifications. The structural integrity of the PP fabric ensures that bags can withstand the rigors of industrial handling, stacking, and long-distance shipping while maintaining their shape and stability.
The Role of Inner Coating in Industrial Protection
The integration of an inner coating, typically consisting of PE or PP lamination, transforms a standard breathable bag into a formidable barrier. This specialized layer is designed to prevent the leakage of fine powders and granules, ensuring that zero product loss occurs through the weave of the fabric.
Beyond leak-proofing, the inner coating serves as a critical moisture barrier. By blocking humidity and external contaminants, it protects the contents from oxidation and clumping, which is particularly vital for chemical powders and fertilizers that are sensitive to atmospheric moisture.
This hybrid design effectively combines the burst strength of woven polypropylene with the sealing capabilities of a polymer liner. Consequently, businesses no longer need to rely on separate plastic liners, which streamlines the packaging workflow and reduces the total amount of plastic waste generated.
Strategic Advantages of Integrated Liner Designs
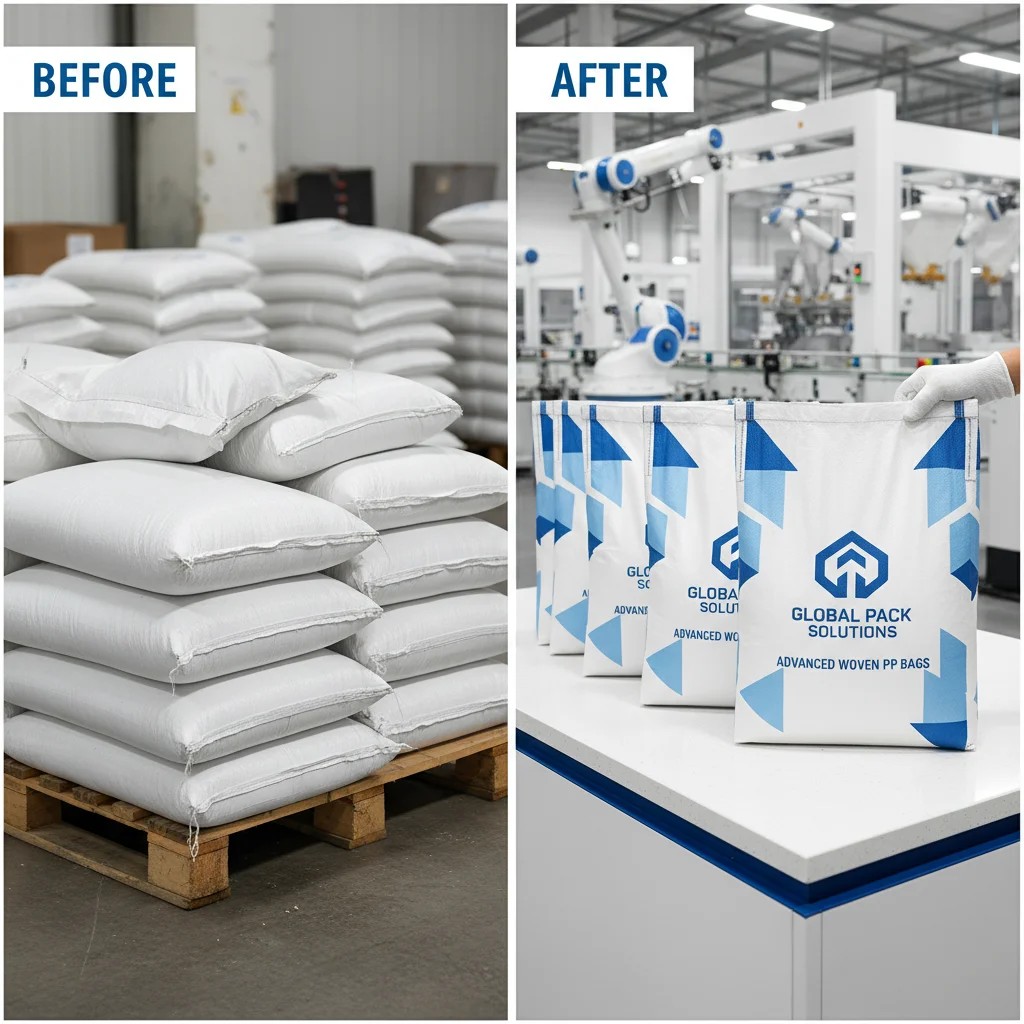
One of the most significant operational benefits provided by a professional pp woven bag supplier is the reduction in packaging labor. Traditional methods require the manual insertion of a PE liner into a woven bag, a process that is time-consuming and prone to error.
By utilizing bags with an integrated inner coating, the filling process becomes significantly faster. This integration not only increases packaging speed but also reduces the total operational expenditure (OpEx) by eliminating the cost of separate liner procurement and the labor associated with their installation.
Furthermore, the smooth outer finish of these coated bags provides a print-ready surface. Whether utilizing BOPP lamination or flexographic printing, brands can achieve high-resolution logos and vibrant colors, ensuring that professional branding is maintained even in harsh industrial environments.
Performance Metrics for Heavy-Duty Packaging
Evaluating the performance of industrial bags requires a data-driven approach focusing on burst strength, coating adhesion, and moisture permeability. A reputable pp woven bag supplier employs rigorous multi-stage testing to ensure that every batch meets international shipping and safety regulations.
When compared to standard woven bags, inner-coated versions show a negligible product loss rate and enhanced shipping stability. These metrics are crucial for companies transporting high-value chemicals where even a small percentage of leakage can lead to significant financial loss or safety hazards.
Packaging Performance Comparison by pp woven bag supplier Standards
Global Applications Across Chemical and Agri-Sectors
The versatility of inner-coated PP woven bags makes them indispensable in the chemical industry, where they are used to transport resins, fine chemicals, and industrial powders. The inner polymer liner acts as a shield against chemical agents, ensuring that the product remains uncontaminated and stable throughout the global supply chain.
In the agricultural sector, these bags are widely used for fertilizers and grains. Because these products are highly susceptible to humidity, the water-resistant inner layer provided by a quality pp woven bag supplier is essential for extending shelf life and preventing oxidation, thereby maintaining the nutritional or chemical potency of the contents.
Sustainability and Recyclability in PP Manufacturing
As global regulations move toward a circular economy, the sustainability of packaging materials has come under intense scrutiny. Polypropylene is a thermoplastic polymer that is 100% recyclable, meaning that both the woven fabric and the inner coating can be processed and repurposed into new plastic products.
Modern manufacturing processes focus on reducing material waste by optimizing the weight-to-strength ratio. By using an integrated coating rather than a separate liner, the total amount of plastic used per unit is reduced, contributing to a lower carbon footprint for the end-user.
Companies partnering with a forward-thinking pp woven bag supplier can now track the recyclable lifecycle of their packaging. This transparency supports corporate green initiatives and ensures compliance with international environmental standards, turning packaging from a waste liability into a sustainable asset.
Quality Control and Customization Standards
Customization is key to achieving optimal packaging efficiency. Every industry has unique requirements for bag dimensions, closure types—such as heat sealing or stitching—and fabric density. A professional pp woven bag supplier offers a dedicated customization hub to tailor these specifications to the exact needs of the client.
Quality control involves rigorous multi-stage testing. This includes tensile strength tests to prevent bursting under heavy loads and coating adhesion tests to ensure the inner liner does not peel or crack during movement. Such precision ensures that the bags can withstand the stresses of automated filling lines and rough handling during logistics.
Furthermore, the integration of inventory tracking and order automation allows for real-time monitoring of stock levels. This ensures that large-scale manufacturing plants never experience downtime due to packaging shortages, creating a seamless flow from production to global distribution.
Comparison of Packaging Solutions Performance
| Bag Feature |
Standard Woven |
Inner Coated Bag |
Performance Score |
| Moisture Barrier |
Low |
Excellent |
9/10 |
| Powder Leakage |
High Risk |
Negligible |
10/10 |
| Packing Speed |
Slow (Manual) |
Fast (Integrated) |
8/10 |
| Burst Strength |
High |
Very High |
9/10 |
| Labor Cost |
Higher |
Lower |
7/10 |
| Recyclability |
100% |
100% |
10/10 |
FAQS
Standard woven bags are breathable and may allow fine powders to leak through the weave. Inner coated bags feature a laminated film layer on the inside that provides a waterproof barrier and prevents fine particles from escaping, making them ideal for materials that require total containment.
Yes, provided the correct resins are used. We offer food-grade PP and PE materials that comply with international safety standards, making these bags suitable for agricultural and food products that require moisture protection without compromising safety.
Absolutely. The smooth finish of the coated bags is specifically designed for high-quality BOPP lamination and flexographic printing. This ensures your brand logos and product information are vibrant, durable, and resistant to wear during shipping.
Since both the outer woven fabric and the inner coating are typically manufactured from the same family of polymers (Polypropylene or Polyethylene), the bags remain fully recyclable within the standard plastic waste stream, supporting corporate sustainability goals.
Our bags are highly customizable to support various weights, typically ranging from 5kg to 50kg. The final capacity depends on the fabric density, the weave specifications, and the closure method chosen during the design phase.
Yes, the inner coating provides a significant barrier against many chemical agents. This makes them the preferred choice for packaging fertilizers, polymer resins, and various industrial chemical powders that could otherwise react with the atmosphere or leak.
Conclusion
Selecting the right packaging solution is a strategic decision that impacts product quality, operational costs, and brand reputation. By utilizing inner-coated PP woven bags from a professional pp woven bag supplier, industries can achieve a perfect balance of structural strength, moisture protection, and cost efficiency, all while maintaining a commitment to 100% recyclability.
As industrial requirements become more stringent and sustainability becomes a mandate, the shift toward integrated, high-performance packaging is inevitable. We recommend auditing your current packaging process to identify where integrated liners can reduce labor and waste, ensuring your supply chain remains competitive and resilient in the global market. Visit our website: www.ssjtpack.com