The global logistics and industrial packaging sector has seen a paradigm shift toward materials that balance extreme durability with precise protective properties. Among these, large woven polypropylene bags have emerged as a cornerstone for transporting bulk materials, providing the structural integrity required for heavy-duty industrial use while remaining lightweight and cost-effective.
In an era of streamlined supply chains, the demand for packaging that minimizes product loss and maximizes shelf stability is higher than ever. Modern advancements in polymer science have transformed these containers from simple sacks into engineered barriers, integrating multi-layer films and specialized coatings to protect sensitive chemicals, minerals, and food-grade powders from environmental degradation.
Understanding the technical nuances of these packaging solutions is essential for businesses looking to optimize their ROI and reduce material waste. By leveraging high-performance large woven polypropylene bags, companies can ensure their products reach the end-user in pristine condition, regardless of the rigors of international transport.

The Engineering Behind BOPP Inner Coated Bags
The technical superiority of our BOPP Inner Coated bags lies in their hybrid construction. By fusing the high mechanical strength of PP woven fabric with a Biaxially Oriented Polypropylene (BOPP) film and a specialized inner coating, we create a packaging solution that is far more than the sum of its parts. This architecture ensures that the bags can withstand immense pressure while remaining impermeable to external contaminants.
This sophisticated layering serves a dual purpose: the outer BOPP film provides a high-resolution canvas for photorealistic printing, while the inner coating acts as a hermetic seal. This eliminates the operational inefficiency of inserting separate PE liners, streamlining the filling process and significantly reducing the overall plastic footprint per unit.
Global Industry Context and Packaging Challenges
In the global movement of chemicals and minerals, product loss due to leakage and moisture ingress is a multi-billion dollar problem. Standard packaging often fails under the stress of stacking or during humidity spikes in maritime shipping, leading to oxidized powders and compromised chemical stability.
Industry standards, including ISO and various food-grade certifications, now demand higher barriers to prevent contamination. The traditional reliance on multiple plastic layers—a woven bag plus a separate liner—not only increases labor costs but also complicates waste management and sustainability goals.
To address these challenges, the industry is moving toward integrated solutions. By merging the barrier and the structure into a single unit, manufacturers can achieve a "leak-proof" status that protects high-value powders and grains, ensuring that the product's chemical composition remains stable from the factory to the end-user.
Defining High-Performance Large Woven Polypropylene Bags
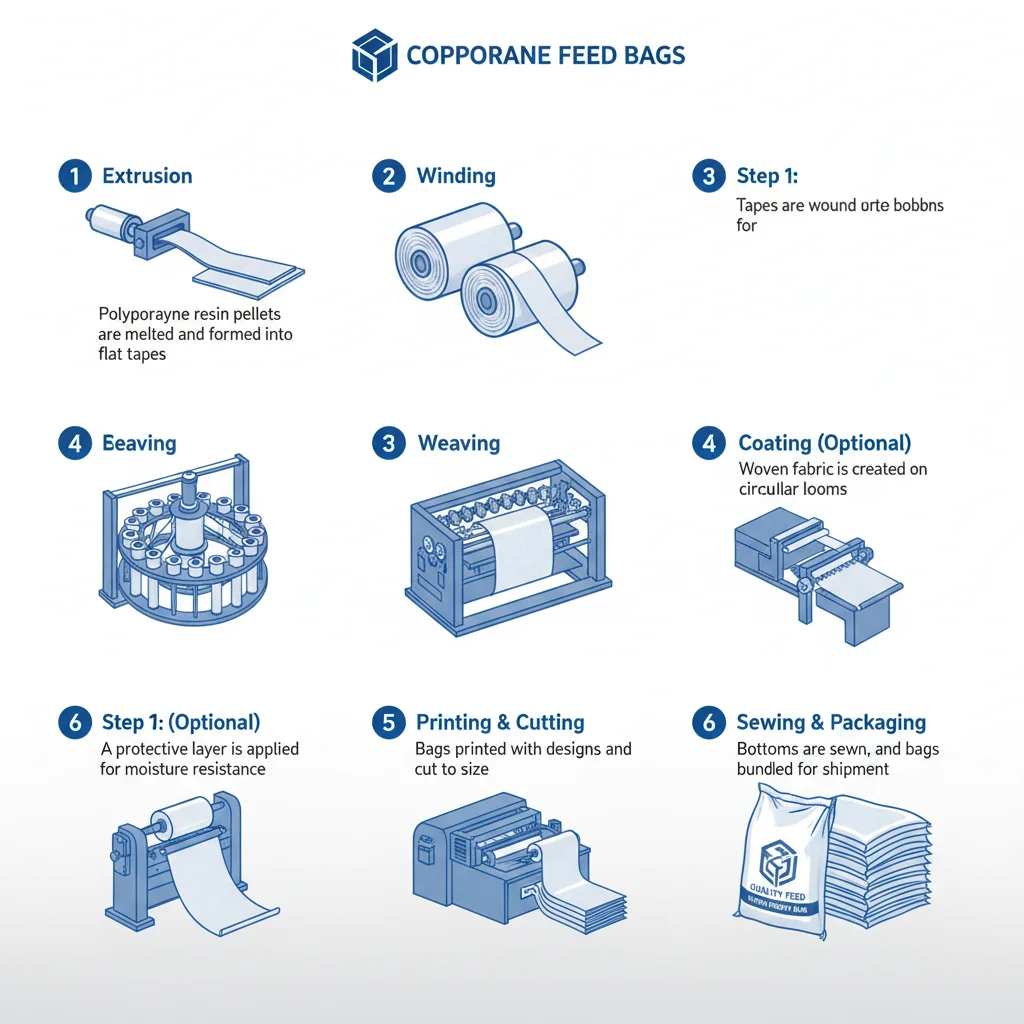
When we discuss high-performance large woven polypropylene bags, we are referring to an engineered textile solution designed for heavy-duty loads. Unlike standard bags, these are constructed from extruded polypropylene tapes that are woven together to create a fabric with exceptional tensile strength and puncture resistance.
The addition of BOPP lamination and an inner coating elevates these large woven polypropylene bags into the realm of "barrier packaging." This means they don't just hold the product; they actively protect it from oxidation and moisture, which is critical for food-grade powders and industrial chemicals.
Ultimately, these large woven polypropylene bags represent the intersection of mechanical durability and chemical protection. They are designed to be compatible with automated filling machines, ensuring that the transition from production to packaging is seamless and efficient.
Core Components of Structural Integrity
The integrity of these bags is derived from four critical factors: the GSM of the PP woven core, the thickness of the BOPP lamination, the quality of the internal moisture-proof coating, and the precision of the closure method. Together, these elements prevent the bag from stretching or bursting under heavy loads, providing a stable footprint for high-stacking in warehouses.
Furthermore, the use of rotogravure printing on the BOPP layer ensures that brand visibility is not sacrificed for strength. The result is a package that is visually premium but structurally industrial, capable of maintaining its aesthetic appeal even after rigorous handling and transport.
Performance Comparison of Packaging Solutions
Global Applications Across Industrial Sectors
These packaging solutions are deployed globally across a variety of high-stakes industries. In the chemical sector, they are used to transport fine powders and resins that would otherwise leak through standard weaves, preventing hazardous spills and product loss. Similarly, in the mineral industry, they protect raw materials from humidity that could cause clumping and processing delays.
In the food and agriculture sectors, the use of virgin, food-grade materials ensures that grains and powdered food ingredients remain uncontaminated and fresh. From remote industrial zones in Southeast Asia to advanced manufacturing hubs in Europe, the reliability of a single-unit moisture-proof bag reduces the complexity of the packaging line and lowers freight costs through optimized packing configurations.
Long-Term Value and Sustainable ROI
The true value of investing in BOPP inner coated bags is reflected in the reduction of the "Product Loss Rate." By moving from a moderate-protection system to a hermetic, inner-coated design, companies see an ultra-low leakage rate, which directly preserves the bottom line.
Beyond the financial gains, there is a significant operational advantage in reducing packaging steps. By eliminating the need for a separate PE liner, companies reduce the labor hours required for bagging and decrease the volume of plastic waste generated during the process.
Finally, the high-end photorealistic packaging enhances brand impact. A professional, vivid exterior signals quality and trust to the buyer, transforming a simple industrial container into a marketing tool that stands out on retail shelves or in B2B warehouses.
Future Trends in Polymer Packaging Innovation
The future of industrial packaging is moving toward "smart" materials and increased circularity. We are seeing a trend toward the integration of UV-protective additives and biodegradable polymer blends that maintain the strength of PP woven fabric while reducing the long-term environmental impact.
Automation is another key driver; the next generation of bags is being designed for even more seamless integration with AI-driven filling and sealing equipment, allowing for zero-touch packaging cycles that further reduce contamination risks.
As global regulations on single-use plastics tighten, the focus is shifting toward "Eco-Efficiency." The transition to unified bags (liner + bag in one) is a first step toward a more sustainable model that uses fewer raw materials while providing superior protection.
Comparative Analysis of Industrial Packaging Performance
| Packaging Type |
Barrier Level |
Labor Efficiency |
Brand Impact |
| Standard PP Woven |
Low |
High |
Basic |
| PP Woven + PE Liner |
High |
Low (Manual) |
Moderate |
| BOPP Laminated |
Medium |
High |
High |
| BOPP Inner Coated |
Ultra-High |
Ultra-High |
Premium |
| Valve Bags |
High |
High (Auto) |
Industrial |
| Custom Hybrid |
Customizable |
Medium |
Variable |
FAQS
Standard PP woven bags are primarily breathable and provide basic structural containment. BOPP Inner Coated bags, however, add a laminated outer film for high-resolution printing and a specialized internal coating that creates a moisture-proof barrier. This integrated design eliminates the need for separate plastic liners, reducing labor and material costs while providing superior protection against leaks and humidity.
Yes, our BOPP Inner Coated bags can be manufactured using 100% virgin, food-grade materials. This ensures that there is no contamination and that the packaging complies with international food safety and packaging standards, making them ideal for grains, sugar, and powdered food ingredients.
By integrating the moisture barrier directly into the bag structure, you remove the need for an additional PE liner bag. This removes the labor cost associated with manually inserting liners into every unit and reduces the amount of plastic waste, leading to a more streamlined and cost-effective filling process.
We utilize high-resolution rotogravure printing on the BOPP film. This allows for photographic images, complex gradients, and vibrant colors that are resistant to peeling and fading. It transforms industrial packaging into a high-impact branding tool that enhances retail visibility.
Absolutely. Our bags are engineered to be compatible with most automatic filling and sealing equipment used in the chemical and plastics industries. Their structural stability ensures they feed correctly through the machinery without jamming or tearing.
Lead times typically range from 15 to 25 days following the final approval of the artwork and specifications. This allows for precision control over GSM, dimensions, and coating thickness to ensure the product meets your exact industrial requirements.
Conclusion
The evolution of industrial packaging has led to the development of BOPP inner coated large woven polypropylene bags as a premier solution for bulk transport. By combining extreme tensile strength with a hermetic internal barrier and premium external aesthetics, these bags solve the dual challenge of product protection and brand visibility. The shift toward integrated, liner-free designs not only reduces operational overhead but also aligns with global sustainability trends by minimizing unnecessary plastic layers.
As industries continue to automate and global supply chains face increasing volatility, the reliability of your packaging becomes a competitive advantage. We recommend upgrading to high-barrier, unified packaging to ensure zero product loss and maximum shelf stability. For more information on how to optimize your industrial packaging, visit our website: www.ssjtpack.com